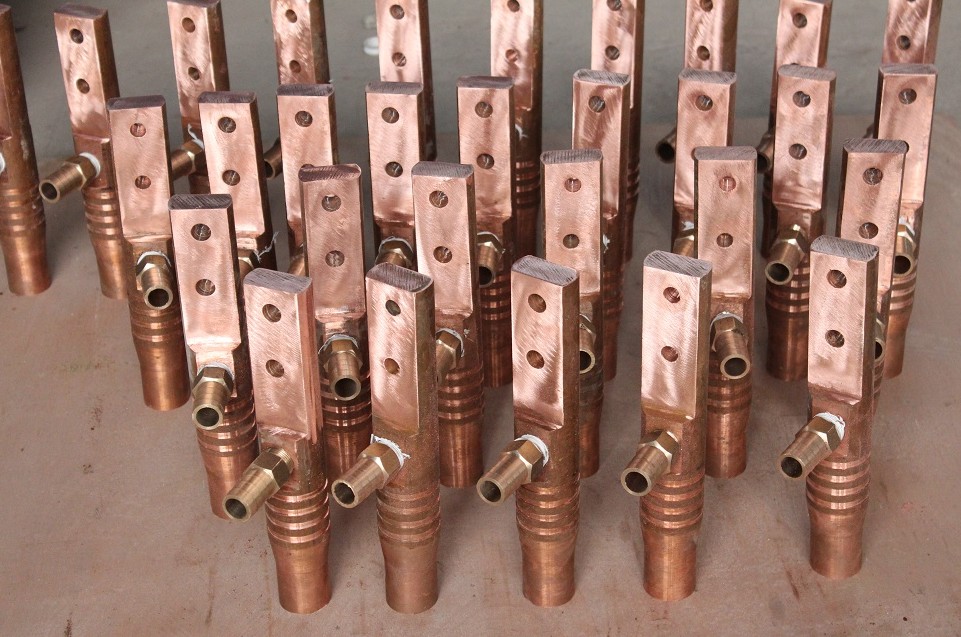
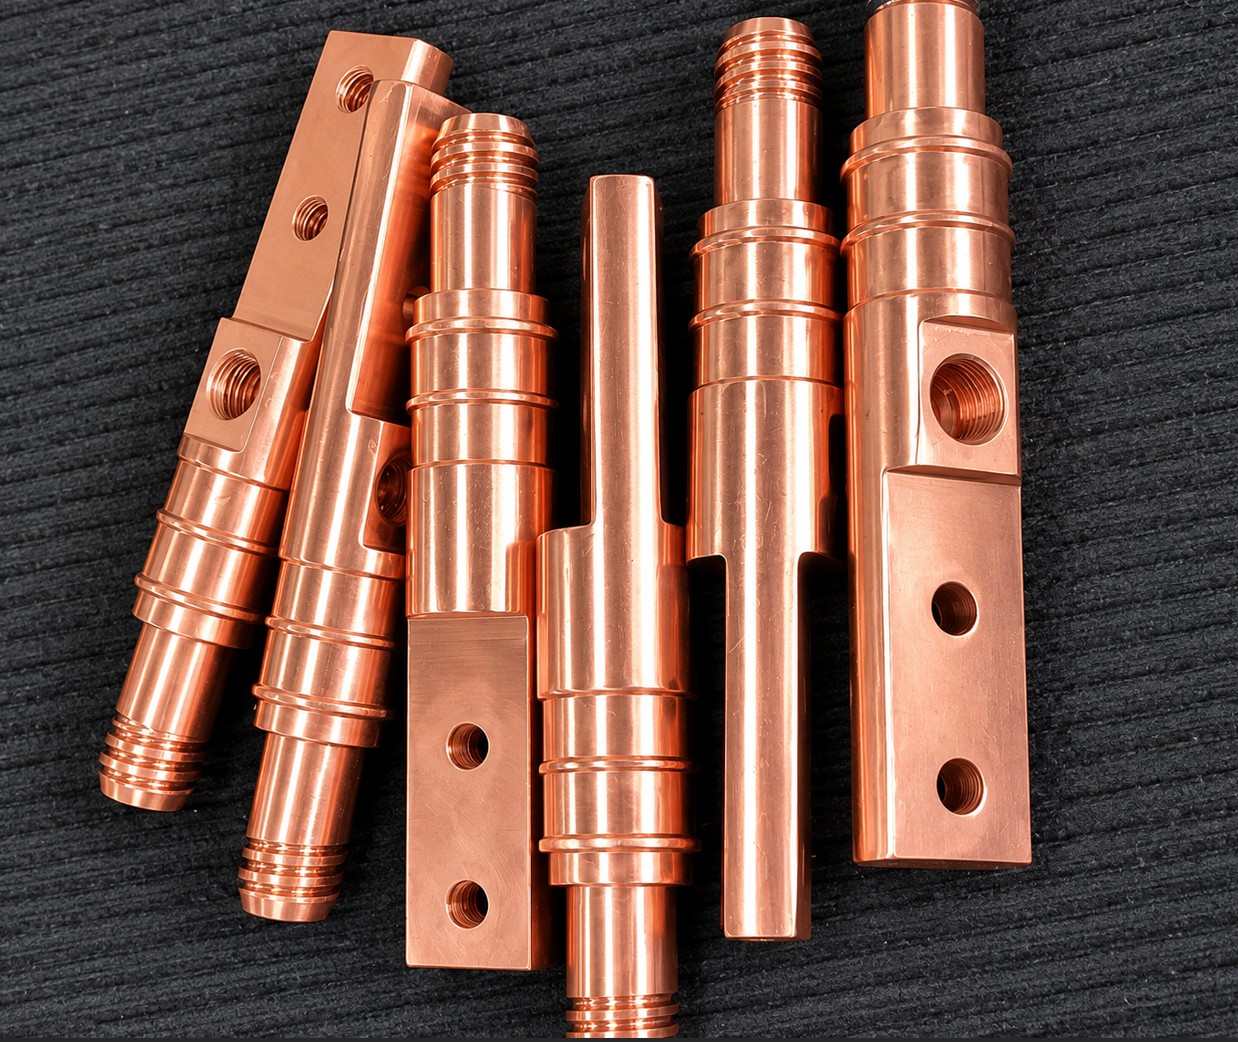
The copper head at the end of a water-cooled cable on medium frequency induction, vacuum and electric arc furnaces. Cold pressed onto the conductor, sealed on a machined taper, and openable with a copper nut when the hose needs replacing.
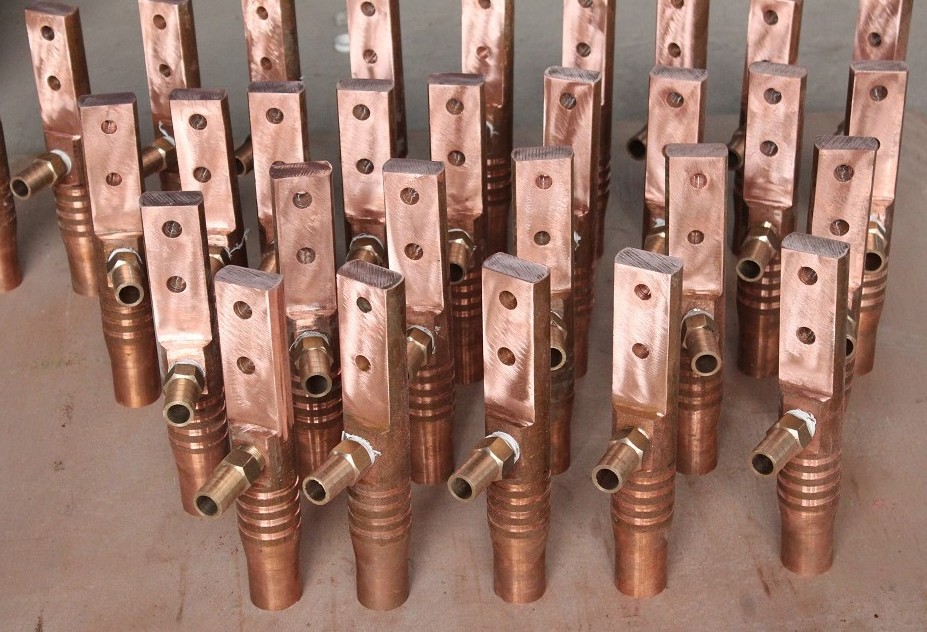
Cable electrode head, water-cooled cable lug, cable terminal head, copper cable end fitting. Dimensions in inches, pull strength quoted in pounds — our joint holds over 17,600 lbf.
Electrode head, cable end fitting, water-cooled cable terminal; Kabelkopf, Elektrodenkopf, tête de câble. Dimensions in millimetres, force in kN — over 78 kN.
Send the electrode head drawing, the cable cross section and the connection dimensions in whichever units you work in. The manufacturing drawing carries both.
The electrode head is joined to the stranded copper conductor by cold press forming — hydraulic crimping with no solder and no pre-heating. The joint is mechanically firm, contact resistance is low, and the individual copper strands are not damaged in the process.
A single joint between one head and the copper conductor withstands a pull of more than 8 t (about 78 kN, 17,600 lbf). That is what keeps the connection between the electrode and the flexible conductor from breaking during repeated furnace tilting and furnace changeover.
Inside the head there is a tapered seat. Tightening the copper nut against that taper makes the electrical connection and seals the water circuit in the same movement. When the rubber hose on the water-cooled cable has to be replaced, you simply unscrew the copper nut on the head — the hose comes off and the copper head is reused.
Design and production are provided as a full service to the customer's requirement.
Click any photo to enlarge.
| Product | Water-cooled cable electrode head |
|---|---|
| Furnace types | Medium frequency induction furnace, vacuum furnace, electric arc furnace |
| Material | High-conductivity copper |
| Cable joint | Cold pressing (hydraulic crimping) onto the stranded copper conductor |
| Joint strength | Each joint withstands a pull of more than 8 t (about 78 kN / 17,600 lbf), so the cable does not break at the electrode during repeated furnace tilting |
| Internal structure | Tapered seat: tightening the copper nut makes the electrical contact and the water seal at the same time |
| Serviceability | Unscrew the copper nut to replace the rubber hose; the electrode head is reused |
| Connection to equipment | Flat pad, flange, thread or taper — to drawing |
| Dimensions | Outside diameter, length, hole pattern, thread and water port all to drawing |
| Surface | Bare copper or tin plated |
| Service | Full design and production service to the customer's requirement |
The pull strength above is the manufacturer's design and test value for a single joint; the figure for your cable size is confirmed with the test record supplied on request.
Melting furnaces that tilt to pour, where the cable and its head flex on every heat.
Vacuum melting and heat treatment plants, with the head matched to the feed-through on the equipment.
High-current connections where the cable moves with the electrode arm.
This page. The copper head itself, supplied loose or cold pressed onto a conductor you send us.
Flat pads, flanges, threaded and coaxial terminals for induction, vacuum, arc and submerged arc furnaces — see water-cooled cable terminals.
Head, conductor, hose and clamps assembled and pressure tested as one unit — see water-cooled cables.
Send the head drawing or photos of the old one, the cable cross section and the connection dimensions. We confirm the geometry and quote with price, weight, lead time and packing.
WhatsApp: +86 188 3715 8450
Email: sales@furnacecopperparts.com